
Ingredients Categories
Finished Products
Finished Food Categories
- Bakery
- Beverages / Juices
- Cereal and grain products
- Confectionery
- Cooking Fats & Oils
- Dairy
- Egg products
- Fruits & Vegetables
- Infant & Baby food
- Meat, Poultry & Fish
- Nuts & Seeds products
- Other Finished Food Categories
- Pet Food
- Plant-based foods
- Prepared foods
- Sauces & Seasonings
- Sweet & Savoury Spreads
Specialised Finished Products
- Bee products
- Biotic products
- Dietary supplements
- Energy drinks
- Functional beverages
- Functional confectionery
- Functional food
- Functional powders
- Meal replacement products
- Nutricosmetics
- Other Specialised Finished Products
- Pet Dietary Supplements
- Pharma and OTC products
- Protein products
- Sugar replacers / Sweeteners
Health & Wellness Areas
Delivery Formats
Operations & Services
- 3D printing
- Analysis/ Testing
- Auditing & certifications
- Blending & mixing
- Bottling
- Certification
- Clinical trials
- Co-packing
- Coating
- Consulting
- Contract manufacturing
- Drying
- Electrospinning
- Encapsulating
- Enzymatic processing
- Extracting
- Extrusion
- Fat structuring
- Fermentation
- Filling
- Flavour development
- Freeze drying
- Granulating/ grinding/ milling / mixing
- High-pressure processing
- Labelling
- Other Operations & Services
- Packaging
- Packet filling
- Pasturising
- Quality assurance
- Saccharification
- Shear cell processing
- Spray drying
- Sterilisation
- Storage & Logistics
- Tabletting
- Toasting / roasting
- Ultra-high temperature processing
Sponsored Content
Developer’s guide: Plant-based product aseptic & extended shelf-life processing
14 Nov 2023
Understanding & addressing plant-based beverages’ process challenges caused by their varied ingredients & characteristics is critical to market leadership in this comparatively young product segment.
Plant-based milks have been around for 100s of years in one form or another, but they started commercially in the 1980s with soymilk. However, it was not until the 1990s that soymilk’s popularity really took off. Now, they are mainstream and have branched out with Rice, Oat, Almond, and many other milks. Manufacturers have also branched out with more beverages like shakes and smoothies, and other products like ice-creams, desserts, cheeses, and spreads.
It seems that since these products parallel their dairy-based counterparts, logic dictates they be processed the same way, but this is not entirely correct. Plant-based products differ significantly from dairy products and each other.
Dairy milk and related products come from a singular source: cows. They have well-defined standards of identity and have been around for centuries. So, we have an extensive knowledge base for processing them. However, plant-based beverages have no defined standards of identity. They are made of a wide variety of ingredients from various fruit and vegetable sources such as;
- Legumes like soybeans and peanuts
- Seeds like almonds and coconuts
- Grains like oats
- Nuts like hemp
These food sources differ significantly and contain varying amounts of fats, proteins, starches, sugars, and minerals. For example:
- Coconut milks are often lower in proteins but can be higher in fats
- Rice milks can be very low in protein but much higher in sugars and carbs
- Almond milks may be lower in proteins and somewhat lower in fats and carbs
- Hemp milks are mid-range for protein but higher in fats and fiber
- Soymilks are higher in proteins and lower in fats
Additionally, developers must add other plant-based ingredients to formulas to meet the expectations of consumers (e.g., taste, texture, nutrition) and manufacturers (e.g., "processability," shelf-life, profitability). Since there is no such thing as a single plant-based milk (or shake, ice cream, etc.) formula, there is no single basic plant-based aseptic or ESL process.
Lastly, plant-based beverages have a comparatively short commercial history. So, developing them is very challenging. Processing these products at commercial conditions accurately while in development is a critical step to successfully bringing them to market.
Aseptic & ESL processing considerations
Low-acid aseptic products must have a 12-log reduction of bacteria. They are commonly processed at 137° to 150°C, with hold times of 1-10 seconds. They must be filled under sterile conditions into hermetically sealed, sterile packages. These products have a non-refrigerated shelf-life of 6 or more months and are good but not necessarily premium quality. In some places (like the USA), aseptic processes and products are highly regulated.
ESL products are much less regulated. The goal of ESL processing is to provide high/premium-quality products with long shelf-lives. They are processed at conditions exceeding pasteurization but short of sterilization (125°-138°C for 1-5 seconds) and filled into clean containers. These products must be refrigerated but will have a shelf-life of 3 to 6 months.
Because plant-based milks and beverages differ, companies must develop processes for each formula. Although we don't know as much about them as dairy products, there are trends for low-acid aseptic and ESL processing that we can use as starting points. Generally, compared to dairy-based products:
- Plant-based proteins are less heat stable and burn on in heat exchangers.
- Thus, steam injection heating tends to be more effective than indirect heating.
- Plant-based products often have higher incoming bacterial loads .
- So, more extreme thermal process conditions are required to achieve shelf-life and safety assurance levels.
- For example, aseptic process temperatures are often above 144°C, and ESL process temperatures are often >121°C with longer hold times.
- Plant-based products are less physically stable due to the composition of their fats and proteins.
- So, they are homogenized at higher pressures.
- Dairy milks: 138-180 bar (2000-2500 psi).
- Nut milks: 130-200 bar (1900-2900 psi).
- Rice and grain milks: 180-250 bar (2600-3600 psi).
- Coconut milks: 190-250 bar (2800-3600 psi or more).
- Plant-based proteins denature easily when heated, causing sedimentation in the bottom of their containers.
- So, they require downstream homogenization rather than upstream.
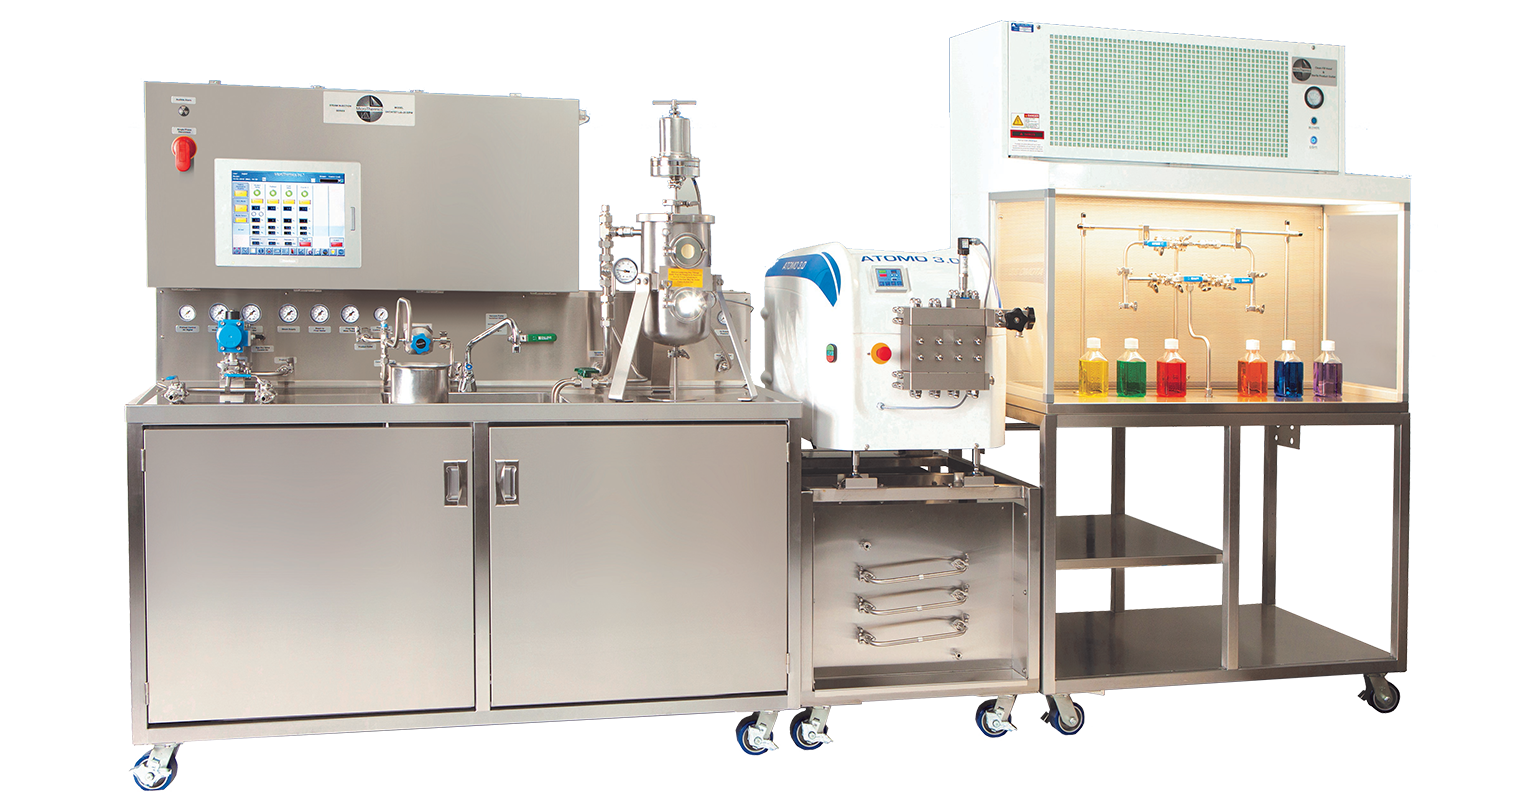
The vast majority of new formulas fail due to processing issues (such as fouling) or not having the required quality after being processed. MicroThermics’ Laboratory UHT/HTST processing systems enable you to quickly and easily process multiple formulas daily, at actual commercial conditions, right in your lab. As the leading supplier for research processing lines, we ensure you can simulate the whole process so you can go from the lab to the plant quickly and efficiently. For more information about processing or our equipment, please visit our website.
- So, they are homogenized at higher pressures.
Companies mentioned
Related categories
Get more of our news on Google
Set Ingredients Network as a 'Preferred Source' to get quicker access to the news you value.
Related news
Fucoidan research surpasses 5000 studies
11 Oct 2026
Global
research interest in the marine extract fucoidan continues to surge, with the
number of published, peer-reviewed papers recently surpassing 5000.
Fi Europe 2026: See you in Frankfurt!
9 Oct 2026
Faravelli continues its centenary celebrations at Fi Europe 2026, looking ahead to what’s next. Meet the team at stand 41K45 and discover the right ingredients to make your products stand out.
Launch of Breakthrough Clean-Tasting Pea Protein Isolate
6 Oct 2026
NUTRALYS® Pea 850F is Roquette’s latest pea protein isolate, representing a breakthrough in delivering a clean, neutral taste for plant-based product formulations.
Read more
The Hybrid Meat Advantage
6 Oct 2026
Hybrid meat is quickly gaining recognition across Europe as a powerful way to meet modern food trends and consumer needs. At Roquette, we help food producers create hybrid meat products that deliver on taste, texture, affordability, and sustainability.
Read more
Turning plant potential into food solutions
1 Oct 2026
Today, plant-based and free-from ingredients must do more than replace. MartinoRossi combines nutrition, functionality, and processing performance to address new formulation challenges.
Read more
Hügli Food Industry: Innovations at Fi Europe 2026
1 Oct 2026
Taste 90 years of culinary mastery at Fi Europe (Booth 41G44), where Hügli will feature chilled Bresc Umami compounds alongside Sauce Culture, its newest snack seasoning concept.
Read more
Nactarome: New possibilities in natural innovation
24 Sep 2026
As food innovation becomes increasingly multi-dimensional, Nactarome's expanding expertise reflects a growing industry focus on integrated natural ingredient solutions.
Read more
A new standard for omega-3 experience
13 Apr 2026
Omega-3 quality is no longer just about purity or concentration. Senses™ by Naturmega delivers ultra-pure, sensory-optimised omega-3 with no taste, no odour, and improved stability.
Read more
PharmaLinea’s iron supplement delivers improvements in hemoglobin comparable to ferrous sulfate with fewer side effects
23 Feb 2026
PharmaLinea, a Slovenian developer and manufacturer of private label food supplements, has announced the completion of a clinical study evaluating its finished formulation for iron deficiency.
Read more
LomaChelateX® – power in magnesium bisglycinate
12 Feb 2026
Gentle and effective: magnesium bisglycinate is setting a new standard. Through its LomaChelateX® brand, Dr. Paul Lohmann® delivers magnesium bisglycinate and a broad range of fully reacted mineral bisglycinates made in Germany.
Read more